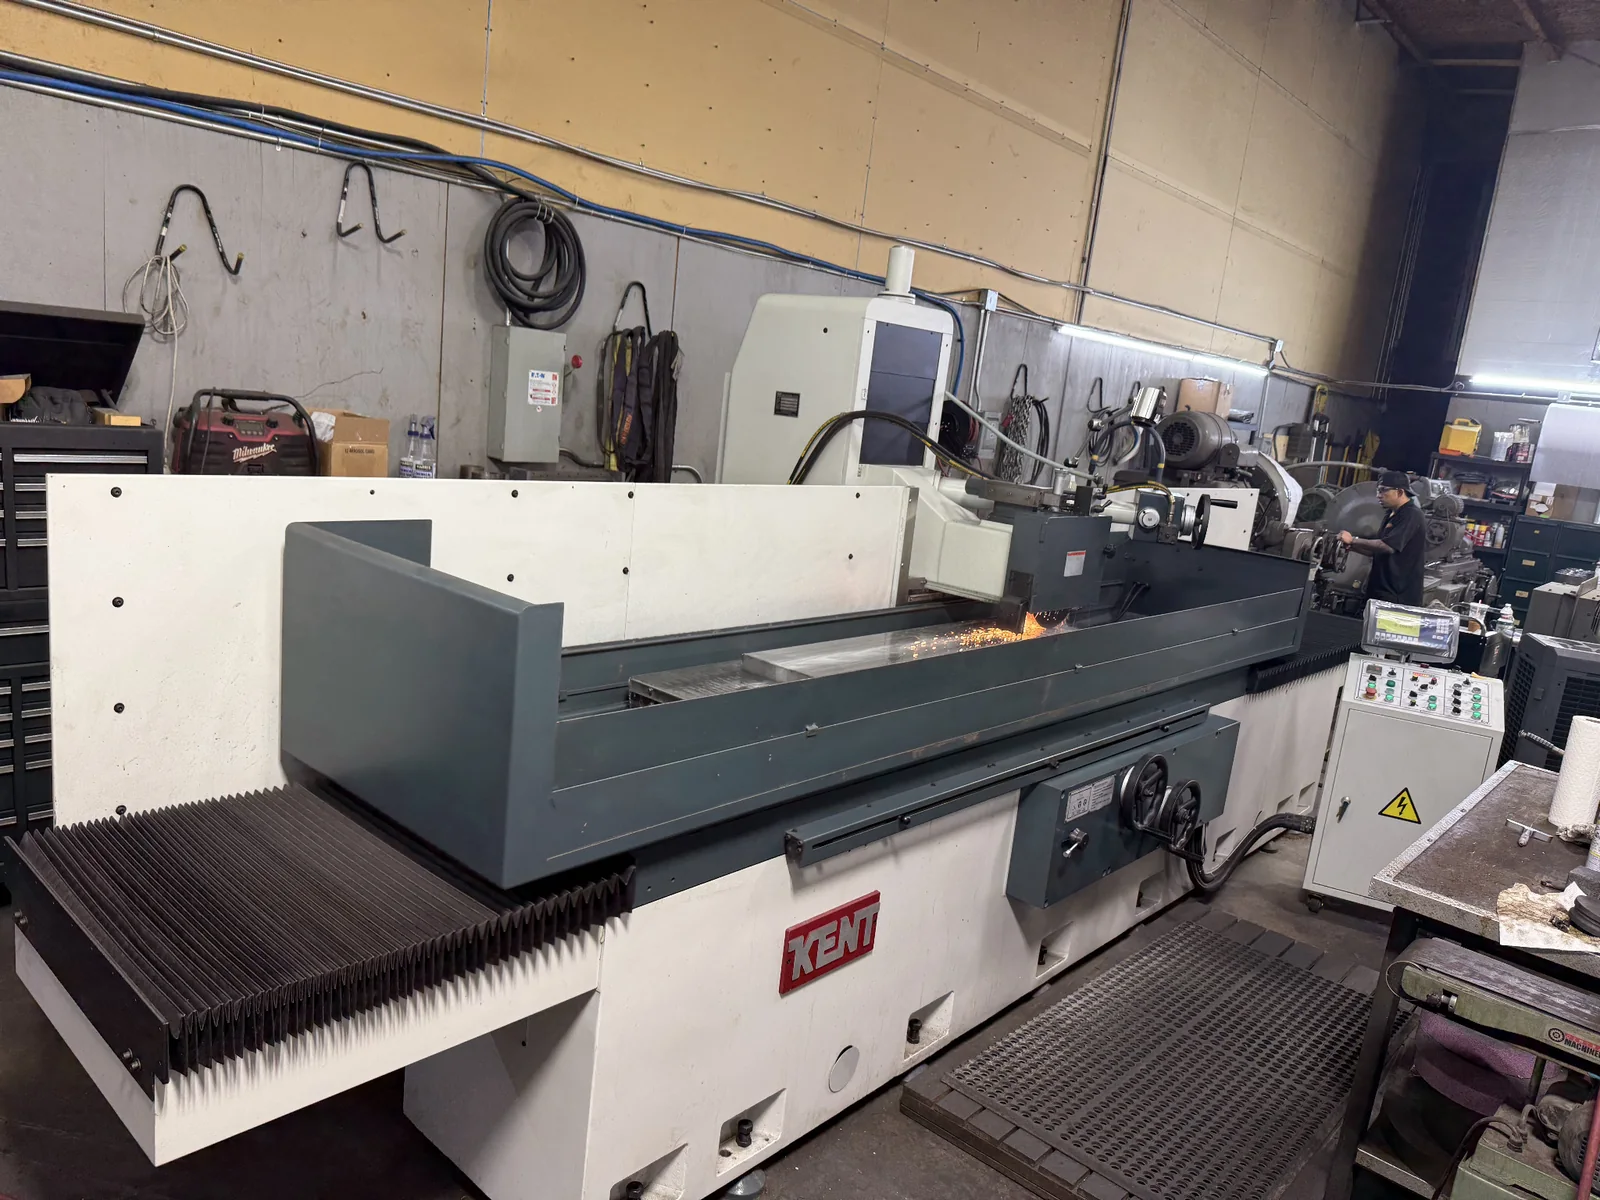
Large flat parts we used to send to other shops now get ground in one setup at our Jones Rd W shop.
Grindmasters now runs a Kent KGS-620AHD precision surface grinder with a 24" x 80" electromagnetic chuck. Before it arrived, jobs this size left the building and went to other shops, gate valve gates among them. Now they stay here. If you have a flat part that has been "too big" for a standard surface grinder, send the drawing and we'll tell you if it fits.
A 24" x 80" Kent, now running at Grindmasters
The KGS-620AHD is a reciprocating surface grinder: the table carries the part back and forth under a horizontal wheel while the column steps across. Ours has the 24" x 80" chuck and automatic downfeed.
What it changes for you is simple. A part that used to need a second shop, or two setups on a smaller chuck, now gets ground end to end in a single setup here in Houston. One setup means one reference surface, and no step where a re-clamped part didn't land quite where it was.
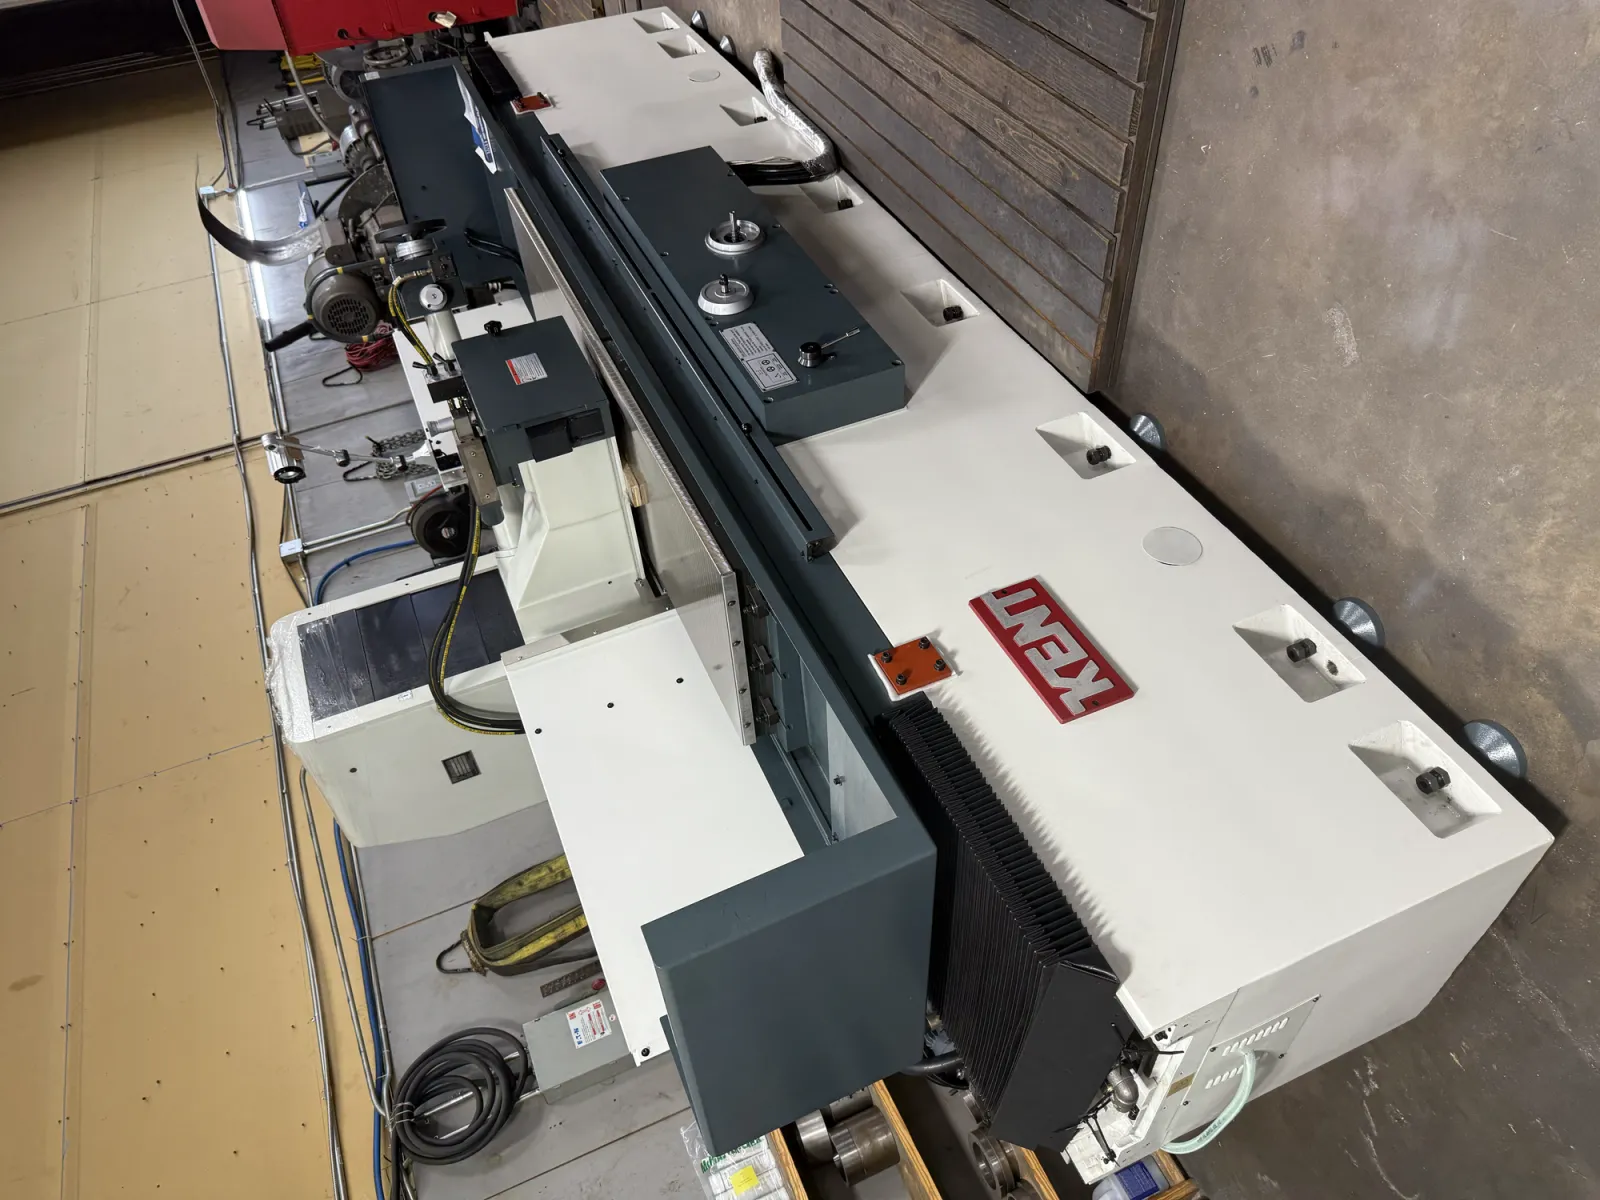
Looking down the length of the Kent KGS-620AHD.
Will your part fit?
Start with length and width, then check height and weight. Those last two trip people up, because the brochure numbers aren't the part numbers.
| Kent KGS-620AHD | |
|---|---|
| Chuck / working area | 24" x 80" |
| Table travel (length) | about 87.7" |
| Crossfeed travel | 26" |
| Spindle center to table | about 23.6" |
| Usable part height | roughly 12" (depends on chuck thickness) |
| Rated table load | 3,300 lb, including the magnetic chuck |
Height. The 23.6" spec is measured from the table to the center of the spindle. The wheel hangs below that center, and the chuck sits on top of the table, so the space your part actually gets is roughly 12".
Weight. The 3,300 lb rating covers everything on the table, and a 24" x 80" magnetic chuck uses a real share of it. A part that weighs close to 3,300 lb on its own is over the limit. Tell us the weight when you send the drawing.
If your part is close on any of these, send it anyway. A drawing answers the question faster than a spec table.
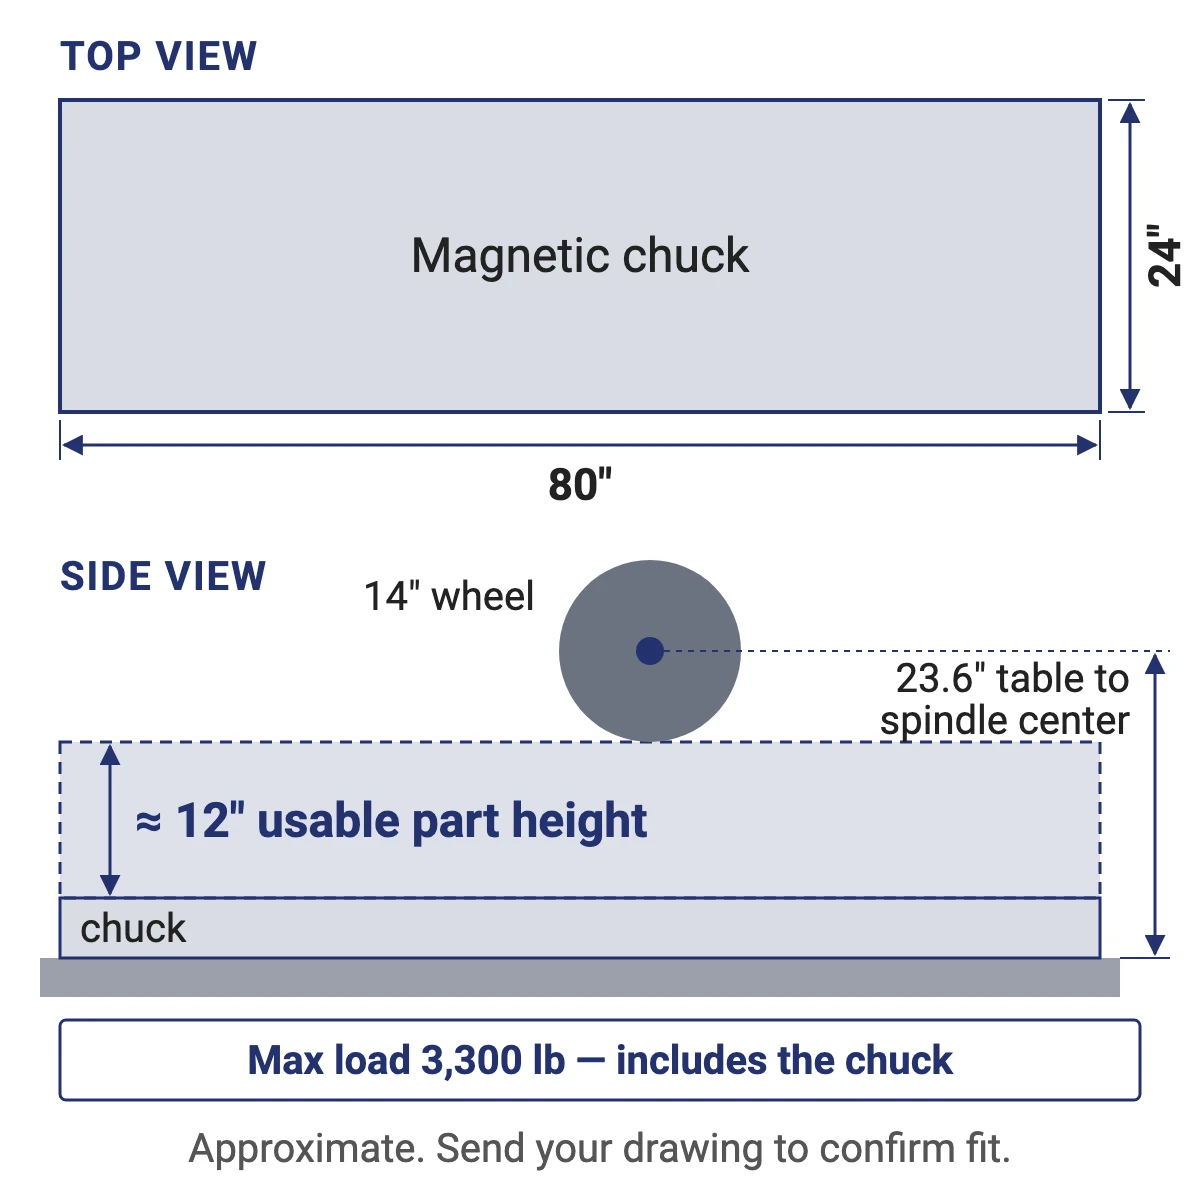
Fit check: footprint, height under the wheel and load limit. Approximate. Your drawing confirms it.
What it's built for
Grindmasters owner Adrian named gate valve work as one of the jobs for this machine, and it's work that used to leave the shop. Gates and seats seal on flat faces, and an 80" chuck has room for one large gate or a row of smaller ones in the same setup.
The rest is what you'd expect from a large surface grinder: long plates and other flat parts that need to come out flat and parallel along their whole length.
The Kent KGS-620AHD at Grindmasters in Houston.
Carbide and hard-coated faces
Yes. We grind carbide and other hard-coated faces on the Kent with diamond wheels. When you send the job, tell us the coating and how much stock comes off per side.
How precise is it?
The handwheel reads in 0.0001" increments, and automatic downfeed steps in from 0.0002" to 0.0016" per pass. It takes a 14" x 2" wheel on a 10 HP spindle.
Those are the machine's numbers, not a promise about your part. Put the tolerance on your print and we'll tell you up front whether the Kent is the right machine for it.
Blanchard or the Kent?
We run both, and they do different jobs.
Blanchard (rotary) grinding is the economical way to take a lot of stock off a big flat surface. It leaves a circular swirl pattern. A reciprocating grinder like the Kent leaves straight-line marks and is the one to use when flatness, parallelism or finish matter more than removal speed (Metal Supermarkets; JLC CNC).
If your part needs a lot taken off and a precise final face, it can go through both: Blanchard to rough it in, then the Kent to finish. If it only needs to be flat and cleaned up, Blanchard alone may be all you need, and it'll cost you less.
Get a large part quoted
Send the drawing through our quote form and include the part's weight and any coating. Or call 713-933-4433. 24-hour service is available when a part can't wait.
Grindmasters Inc., 11203 Jones Rd W, Houston, TX 77065. More on our surface grinding services.
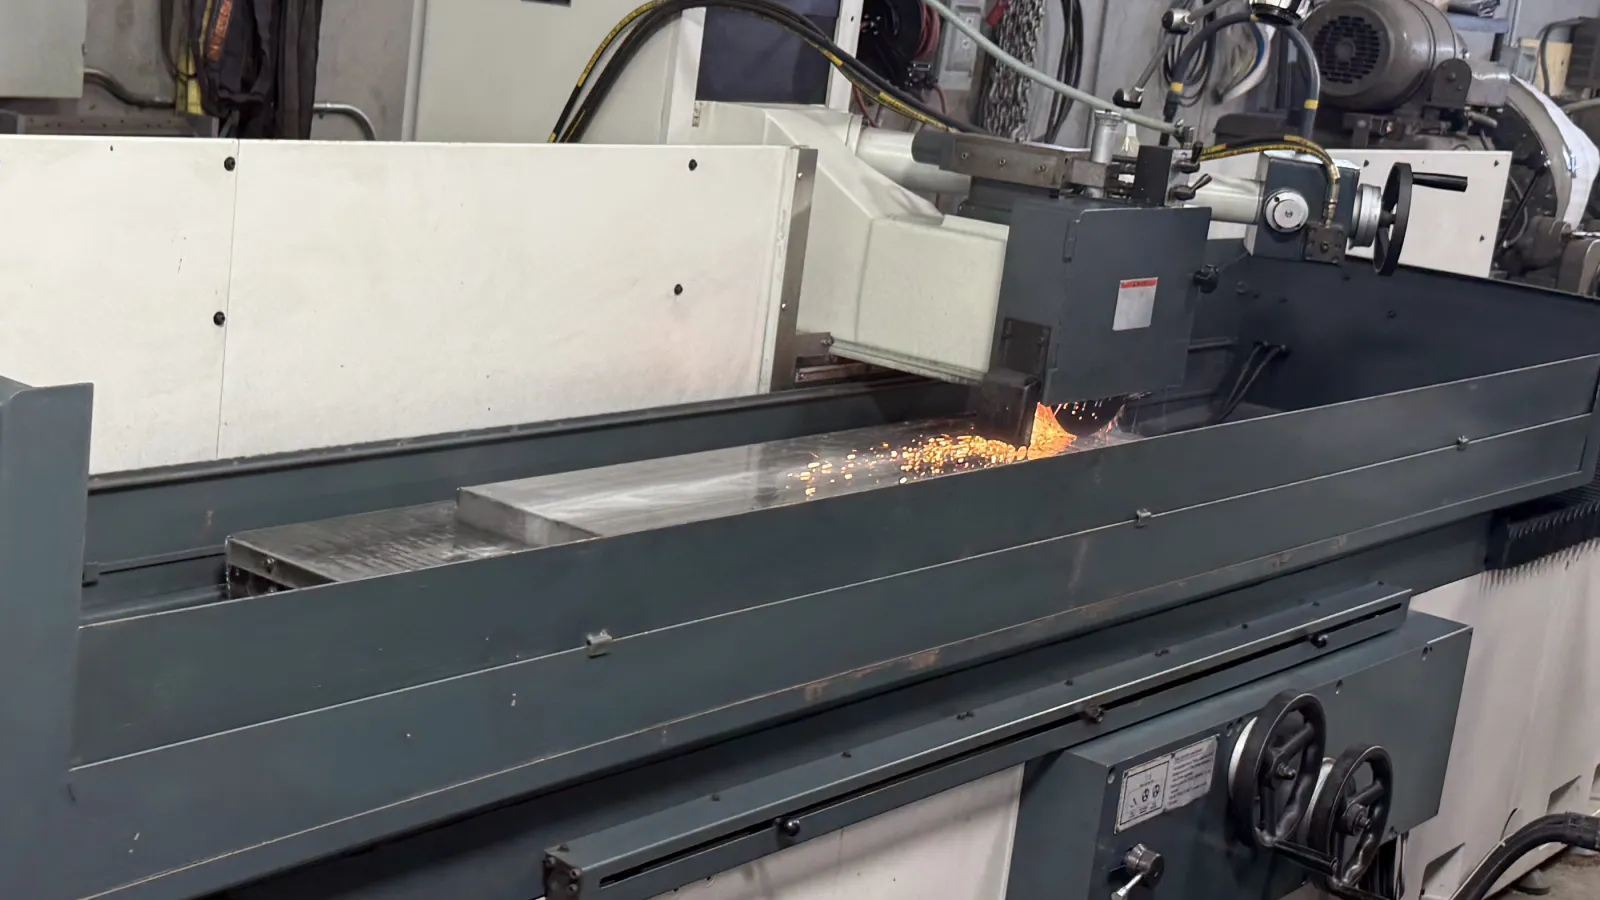
A flat part mid-grind on the Kent.